The battery material recycling line emission standards define the gas cleaning, the dust control and the monitoring that the plant must install, and those three items change both the capital and the value of the product. You, as a recycling company manager or as a project investor, examine the battery material recycling line emission standards together with the specification of the refiners. The air pollution control equipment then becomes part of the process rather than an add-on.
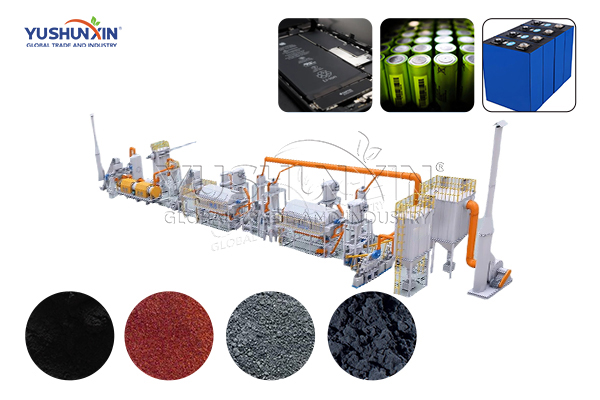
Which standards apply to a battery recycling line?
The particulate limit of the shredding area, the volatile limit of the thermal stage and the effluent limit of the hydrometallurgical section form the three standards that the permit lists. A compliance value of a battery material recycling line review maps each standard to the equipment that satisfies it, because a missing item delays the licence. You confirm the local limit with the authority before the order. The design then covers the full obligation.
How does compliance change the product value?
A plant that documents its emission performance sells to buyers who audit their supply chain, and those buyers pay a premium for a traceable material. An emission standards for battery recycling study also examines the impurity limits of the refiners, because a dirty product loses value even when the emission record is clean. You sample the product and the stack in the same shift, and the two records support each other. The contractual price then reflects both.
Which equipment provides the control?
A cyclone and a bag filter capture the dust of the shredder, and a scrubber removes the acid components of the thermal gas. A pyrolysis disposal emission control design also monitors the pressure drop of the filter, because a clogged bag reduces the airflow and lets the dust settle. You keep a spare set of bags on site, and that stock avoids a stop. The plant then stays inside its limit during every shift.
How does the plant document the result?
A monitoring plan with the sampling points, the frequency and the record format answers the questions of the inspector. You keep the laboratory results and the operating log in one file, because the auditor reconstructs the year from those sources. The plant that publishes a summary to its neighbours reduces the complaints that a new facility often receives. The authority then renews the permit with evidence.
Conclusion for recycling companies and project investors
Compliance protects the value of a battery recycling line through the permit, the control equipment and the monitoring record, and a documented plant sells at a better price. A battery line compliance advisors team that supplies the permit matrix, the treatment layout and the reporting template helps the operator protect both the licence and the margin. The supply of spent batteries keeps growing, and the compliant plant captures the buyers who require an audited source. If your team needs a reference for the process route and the compliance scope, you can learn more about https://www.sxlbp.com/technology/hydrometallurgical-lithium-battery-recycling-plant/ before the next permit review.